
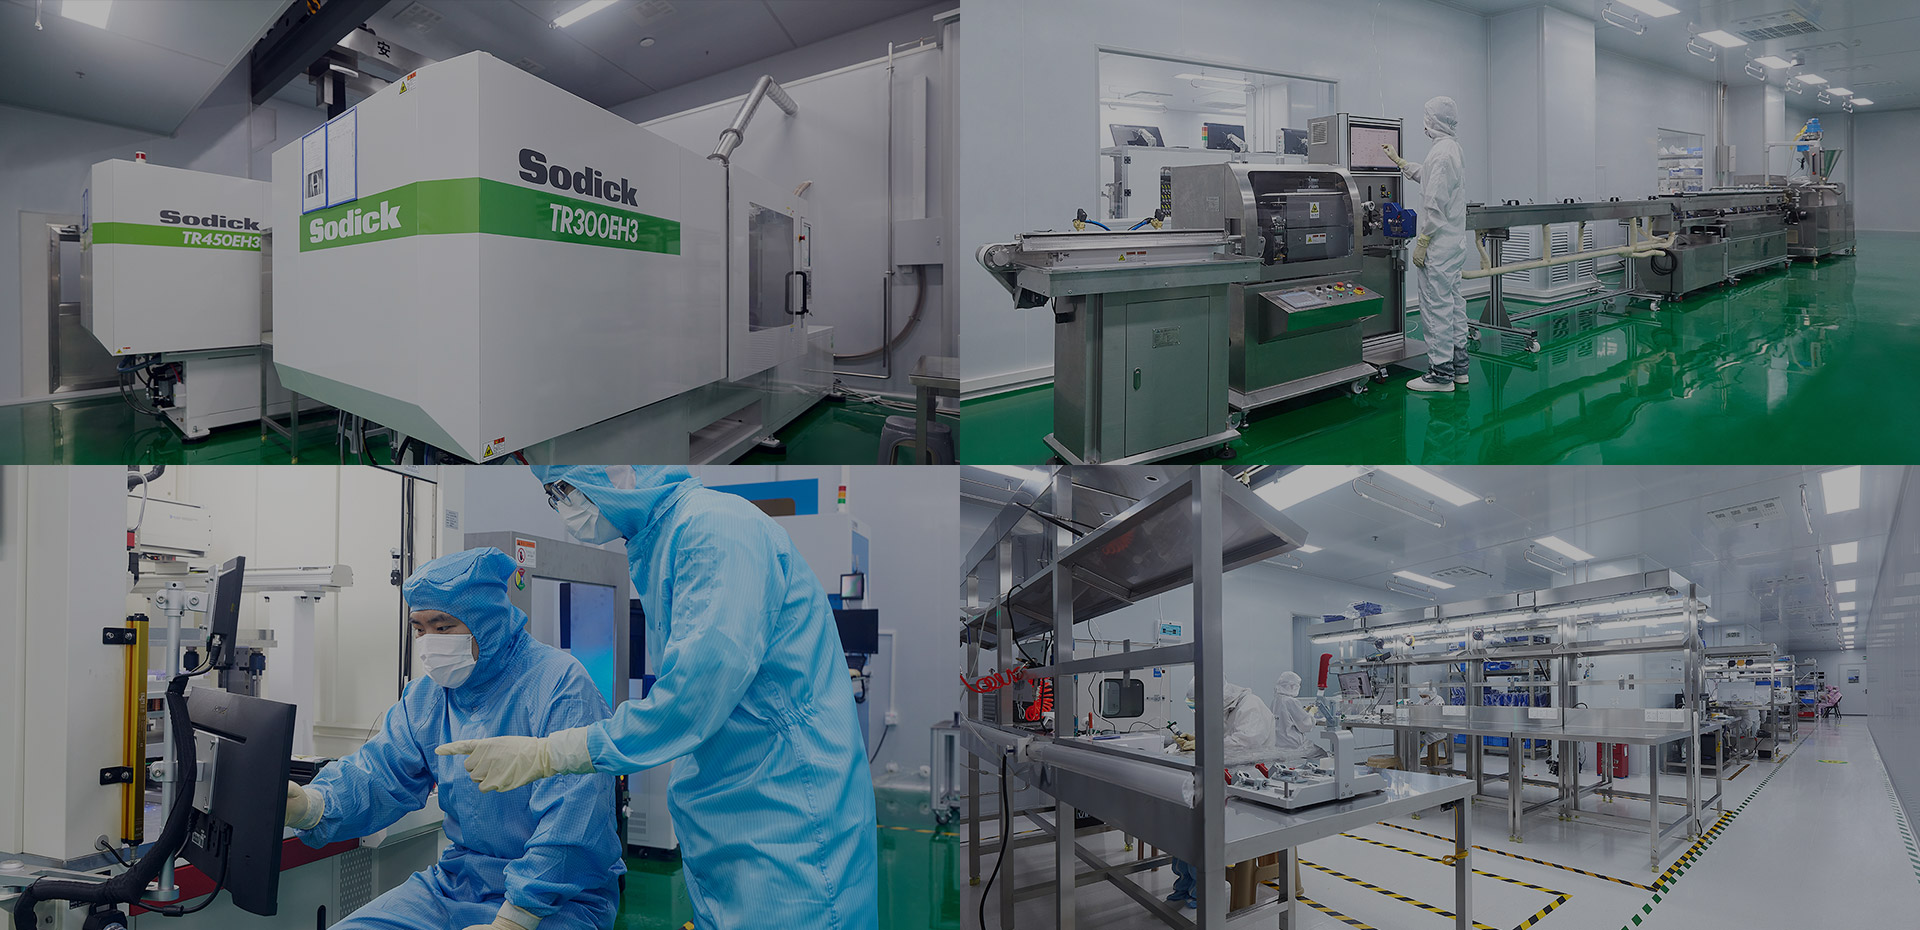
Problem diagnosis and scope
Air leak tests fail silently when test design mismatches the failure mode: a pressure-decay threshold set for package-level leaks misses microchannel porosity, and a bubble test finds cosmetic vents but not functional flow paths. This analysis focuses on pinpointing why specific air-leak methods fail during release and validation stages, with attention to outsourced production and how that affects controls for medical device contract manufacturing. The problem-driven goal is simple: tie each observable failure back to a measurable test variable and a controlled corrective action.
Evidence, expertise, and the industry anchor
Hands-on experience informs the recommendations below: teams with a decade-plus of bench work and fixture design report consistent root causes when they present findings at events such as MD&M West. Practical testing experience, method validation records, and traceable calibration logs build the authoritative basis for choosing tests; our protocol development aligns with industry best practices for medical product manufacturing. Expect explicit acceptance criteria, documented uncertainty, and supplier audit trails as part of a defensible quality program.
Core failure modes that invalidate air-leak testing
Fixture leakage and poor sealing between test interface and part. Test-volume masking: large internal volumes reduce pressure-change sensitivity and permit small but critical leaks to fall below detection limits. Temperature and barometric drift producing false positives/negatives. Incorrect test thresholds that don’t map to functional failure (setting detection to a pass/fail number that lacks engineering justification). Sampling bias: testing only prime parts or visually acceptable samples. Lack of traceable calibration of reference leaks and transducers.
Choosing the right test method — technical criteria
Select based on required detection limit, part volume, material permeability, geometry, and throughput. Helium mass spectrometry: highest sensitivity (suitable when targets demand 10^-8–10^-9 mbar·L/s detection), but requires vacuum chambers and gas handling. Pressure-decay: versatile for inline and bench testing; sensitivity scales with test volume and sensor resolution (appropriate when required detection sits in the 10^-5–10^-3 mbar·L/s range after accounting for geometry). Vacuum-decay (or gross-leak vacuum) balances test speed and sensitivity for small flexible components. Sniffing or tracer-gas sniffers fit localized leak detection during debugging. Choose non-destructive modes when parts must be released to production, and destructively validate margins on sacrificial samples when necessary.
Validation specifics and common measurement mistakes
Define a validation matrix that ties leak-rate limits to functional risk and bench-level impact. Calibrate transducers and reference leaks with traceable certificates; record drift, hysteresis, and resolution. Quantify test sensitivity by calculating minimal resolvable leak (MRL) = sensor resolution / effective test volume, then verify with reference leaks. Avoid single-point pass/fail validation: use multi-rate checks across expected leak magnitudes. Watch for temperature-induced pressure swings; stabilize parts and equipment or compensate with temperature correction. Do not reuse fixtures with wear that changes dead volume or sealing force—document fixture life and replacement criteria.
Implementation checklist for reliable deployment
1) Map each potential leak path to the chosen test method and document why the method detects that path. 2) Produce a validation protocol with reference leak levels and acceptance criteria tied to functional risk. 3) Use control charts for daily instrument performance and reference-leak verification. 4) Train operators on fixture seating force, torque values, and alignment to prevent interface leakage. 5) Log environmental conditions and correct for them in the test software. 6) Perform periodic round-robin tests between suppliers or lines to detect inter-facility drift. 7) Maintain spare parts for fixtures and sensors on a defined maintenance schedule.
Synthesis and practical resolution
Fixes follow the diagnostic logic: reduce test volume to improve sensitivity, tighten fixture interfaces to remove false leakage, validate thresholds to correlate with functional failure, and institutionalize calibration plus operator discipline. For complex assemblies where method choice and fixture engineering intersect with supplier controls, experienced partners that combine fixture design, validation protocols, and production execution reduce escapes — organizations such as kingsin routinely embed those elements into manufacturing flows so test outcomes directly reflect functional integrity rather than sampling artifact.